

How to Choose a Rebar Coupler Manufacturer
A reliable rebar coupler manufacturer can show that its couplers fit your bar sizes and grades, meet the standards in your plans, and have test results to back up their performance. Before you order, ask for product test reports, batch traceability, installation instructions, and the tools each coupler requires.
Couplers join bars end to end without the overlap needed for a lap splice. That can save steel and leave more room for concrete to flow around crowded reinforcement. The list ahead will help you compare manufacturers on those practical points, not just price.
I’m Jordan Harris, a Tennessee-licensed structural engineer who has worked on large concrete and steel projects. I use that experience to focus this guide on the questions I’d ask a rebar coupler manufacturer before a pour.
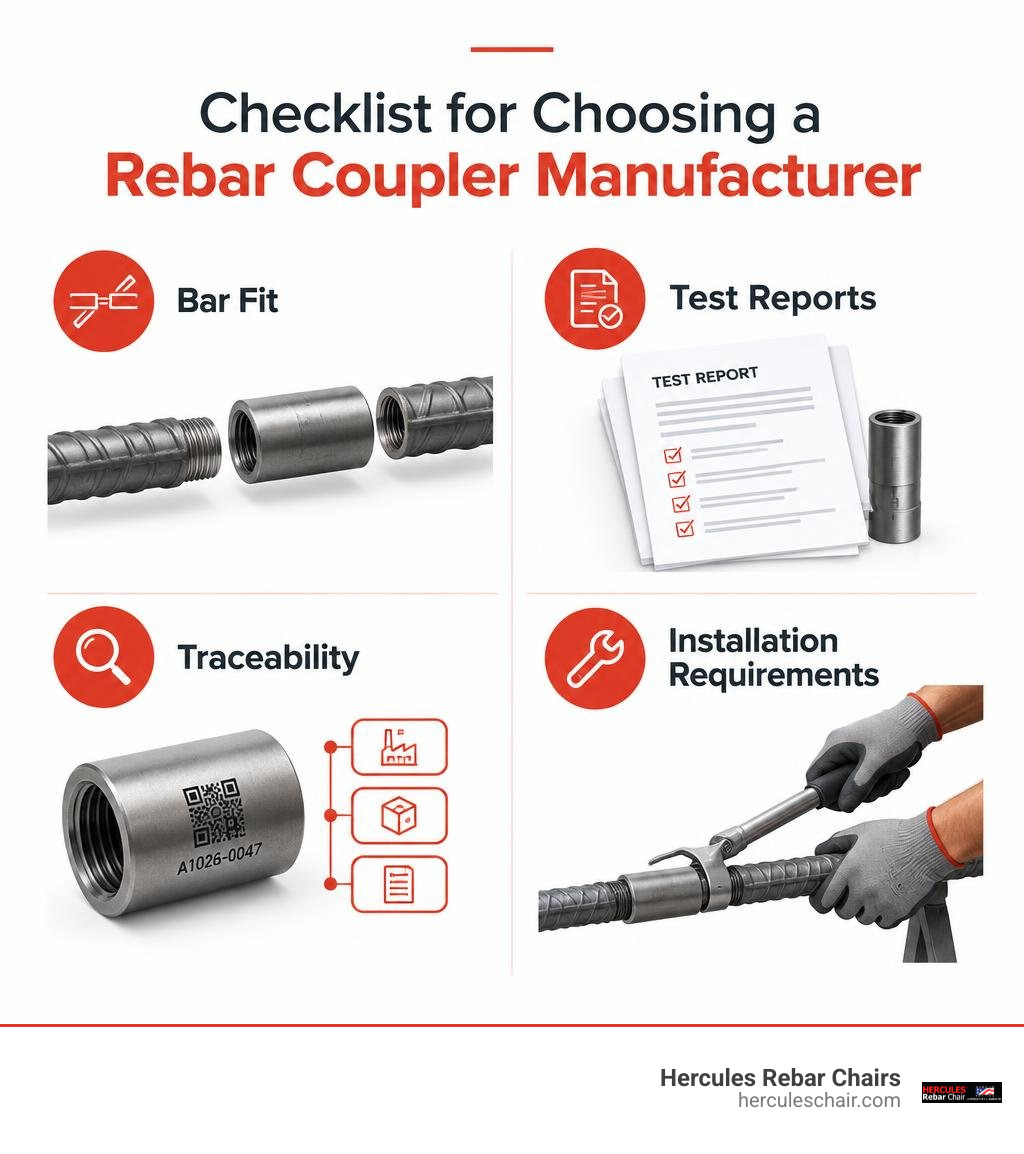
Simple rebar coupler manufacturer glossary:
Why Partnering with the Right Rebar Coupler Manufacturer Matters for Structural Integrity
Reinforced concrete depends entirely on predictable load transfer between steel bars and surrounding concrete. When you connect reinforcing steel, the joint must provide structural continuity under heavy static loads, dynamic cyclic forces, and seismic shifts. Selecting the right fabrication partner ensures that every mechanical joint performs as an unbroken, continuous bar rather than a localized point of structural failure.
Engineering design standards and technical manuals outline strict criteria for continuous load paths. When mechanical splices fail to meet these parameters, load paths break down, jeopardizing structural safety during seismic events or peak structural loads.
Mechanical Couplers vs Traditional Lap Splicing
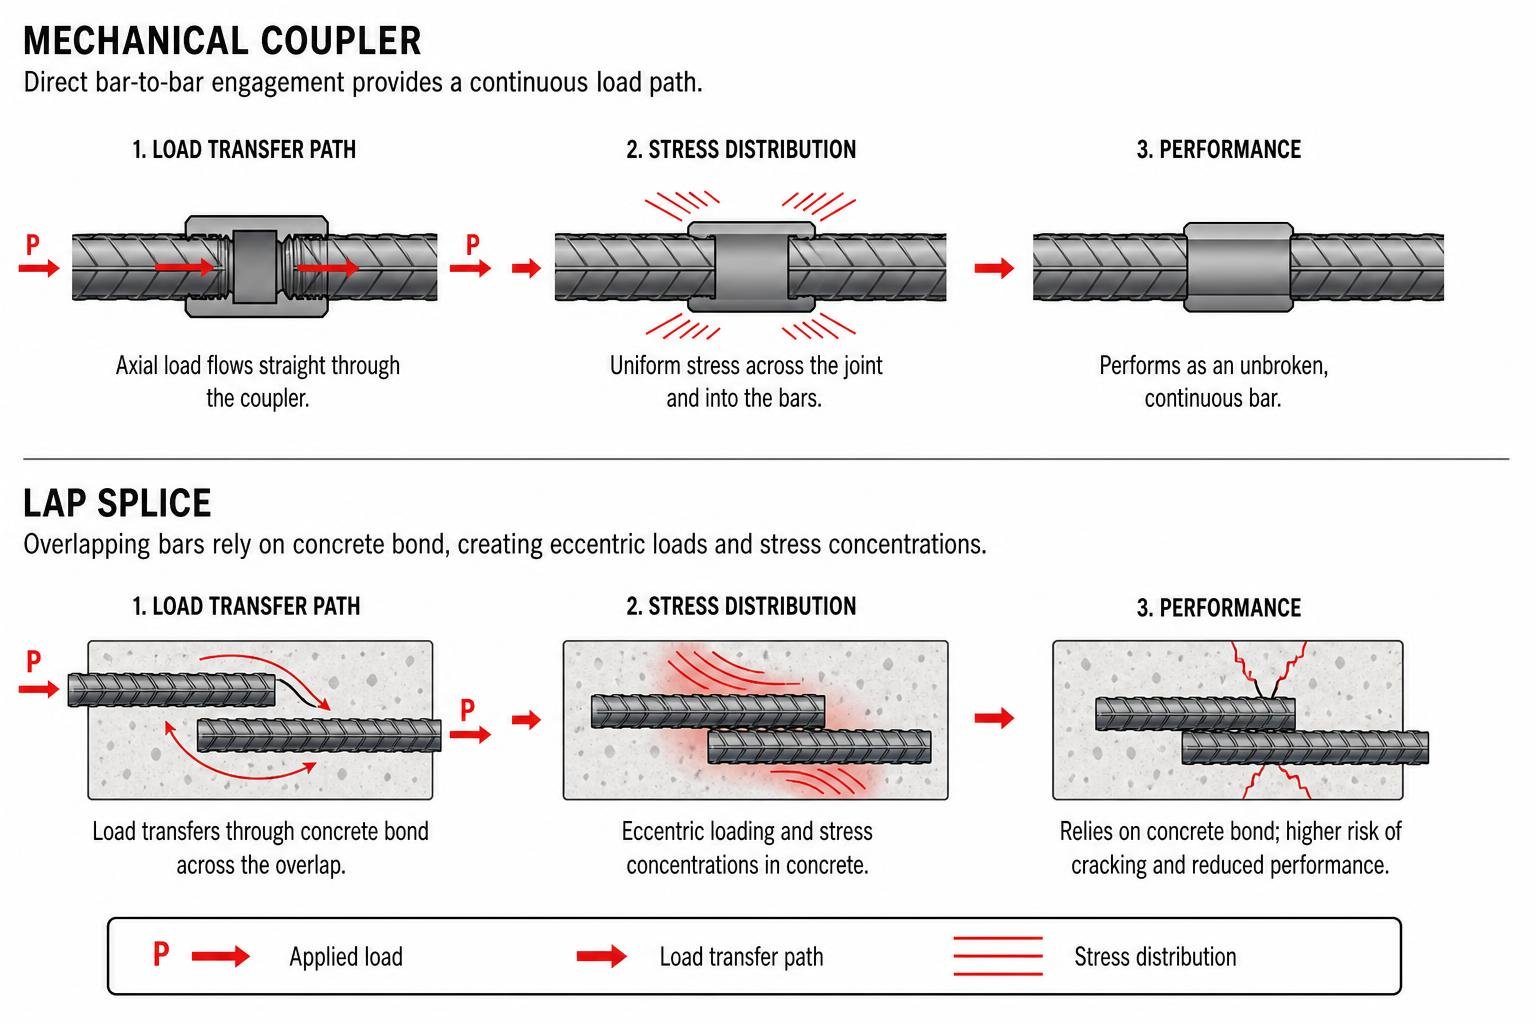
Lap splicing has been the default method for joining rebar across construction sites for decades. However, overlapping two bars relies completely on concrete bonding to transfer load from one bar to another. This reliance introduces eccentric loading and sharp stress concentrations into the surrounding concrete matrix.
Eliminating overlapping steel bars resolves several key engineering bottlenecks:
- Congestion Relief: Lap splices double the steel volume at joint locations, creating dense cages where aggregate cannot pass. Mechanical splicing eliminates this bottleneck, allowing aggregate to flow freely and eliminating air pockets.
- Direct Load Paths: Mechanical couplers connect bars end to end along a single continuous axis, transferring both tension and compression loads directly through the steel rather than relying on concrete shear strength.
- Full Strength Splices: High-performance mechanical connections exceed 125% to 160% of the bar’s specified yield strength, ensuring failure happens in the parent bar rather than the joint.
To maintain code compliance across complex foundation and column layouts, contractors often rely on A Comprehensive Guide to Bar Splices in Construction to determine when mechanical options are legally required over lap joints. When you splice it right with mechanical couplers, your crew avoids the congestion and eccentric loading inherent to overlapping bars.
Steel Savings and Material Efficiency
Lap splices waste substantial amounts of expensive reinforcing steel. Depending on bar diameter, concrete compressive strength, and structural seismic zoning, lap lengths often range between 40 to 60 times the bar diameter. On heavy infrastructure projects using #11 (36 mm), #14 (43 mm), or #18 (57 mm) bars, lap splices can consume 6 to 10 feet of extra rebar at every single connection point.
By cutting out unnecessary overlap, contractors eliminate thousands of pounds of steel per structural floor. For a detailed breakdown of structural load optimization, check out Rebar Couplers: Your Ultimate Guide to Connecting Steel Strong.
Comprehensive Review of Mechanical Splicing Systems
Different structural configurations call for specialized connection methods. A premier manufacturer provides a wide spectrum of mechanical splices suited for cast-in-place pours, precast modular connections, bridge retrofit tasks, and congested column splices.
Technical Capabilities of a Quality Rebar Coupler Manufacturer
To preserve the net tensile area of reinforcing steel, fabricators employ specialized equipment and cold-working techniques. When threading a standard rebar directly, cutting away metal reduces the bar’s cross-sectional area, creating a weak point at the root of the threads.
Top-tier manufacturers overcome this limitation using advanced manufacturing methods:
- Cold Forging and Bar Upsetting: The rebar end is hydraulically compressed without heat, enlarging its diameter so that subsequent thread rolling maintains an effective cross-sectional area equal to or greater than the original bar.
- Rib Peeling and Roll Threading: The outer ribs of the rebar are mechanically shaved down to a uniform diameter before high-pressure rollers displace the metal to form cold-worked ISO metric threads.
- High-Precision CNC Machining: Coupler sleeves are turned from high-strength carbon or alloy steel stocks with minimum tensile strengths reaching 600 MPa or higher.
To achieve precise fit-ups in the field, fabricators rely on specialized equipment detailed in The Heavyweight Champion of Construction: Choosing a Rebar Coupling Machine.
Coupler Varieties from Parallel Threaded to Shear-Bolt Systems
Gaining a complete understanding of different rebar coupler types ensures you pick the right connection system for your specific engineering and assembly needs:
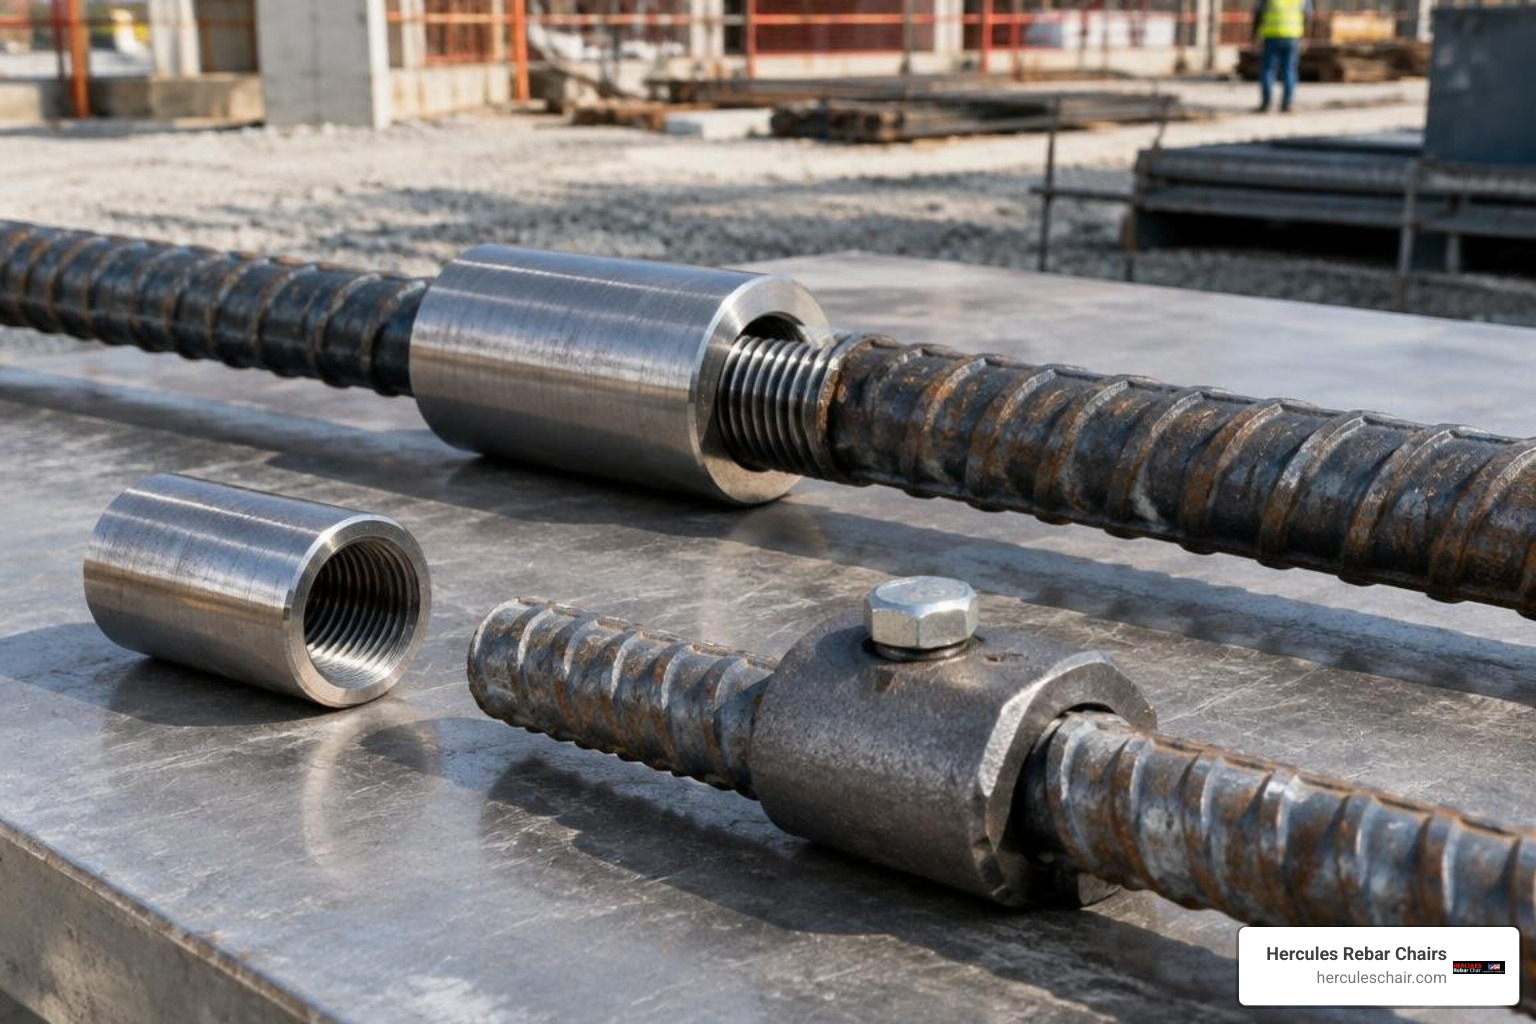
- Parallel Threaded Couplers: These standard sleeves feature internal female threads matching cold-rolled rebar ends. Standard threaded rebar couplers provide fast, repeatable torque-controlled connections for bars that can rotate freely.
- Cold Forged Couplers: Made using upset bar ends, these sleeves achieve full tensile transfer with compact wall thicknesses (often around 7.5 mm), minimizing outer dimensions while preserving 100% bar capacity.
- Transition Couplers: Engineered with dual interior thread pitches or stepped diameters, these specialized units connect mismatched bar sizes (such as splicing a #11 column dowel to a #9 upper-level bar).
- Bolted Shear-Bolt Couplers: Ideal for retrofits, precast tie-ins, and repairs, these sleeves slip over plain-end deformed bars. Workers tighten integrated lock-shear bolts until the hex heads shear off at a predetermined torque, locking the bar in place without prior threading.
- Grout-Filled Sleeves: Widely used in precast column-to-foundation connections, these sleeves feature one threaded end and one wide grouted cavity filled with high-strength, non-shrink structural grout.
| Coupler Type | Bar Size Range | Bar End Prep Required? | Common Applications | Key Benefit |
|---|---|---|---|---|
| Parallel Threaded | #4 to #18 (12–57 mm) | Rib peeling & roll threading | Cast-in-place columns, beams, slabs | Fast assembly with standard calibrated wrenches |
| Cold Forged | #4 to #14 (12–40 mm) | Cold upset forging & threading | High-rise cores, seismic frames | Zero reduction in parent bar tensile area |
| Transition | Multi-step combinations | Size-specific roll threading | Multi-story vertical bar size reductions | Eliminates messy lap splices between differing sizes |
| Shear-Bolt | #4 to #18 (12–57 mm) | None (plain cut bar) | Field repairs, retrofits, bent bar fixes | No bar-end prep machinery required on site |
| Precast Grouted | #5 to #18 (16–57 mm) | Threaded one side / Grouted cavity | Modular precast wall and column joints | Accommodates generous structural placement tolerances |
Quality Standards and Engineering Specifications for Coupler Selection
Never gamble on uncertified connection hardware. Structural engineers require verification that mechanical splices will perform reliably under live loads, dead weights, wind buffeting, and seismic shocks.
Standards and Certifications Every Rebar Coupler Manufacturer Must Meet
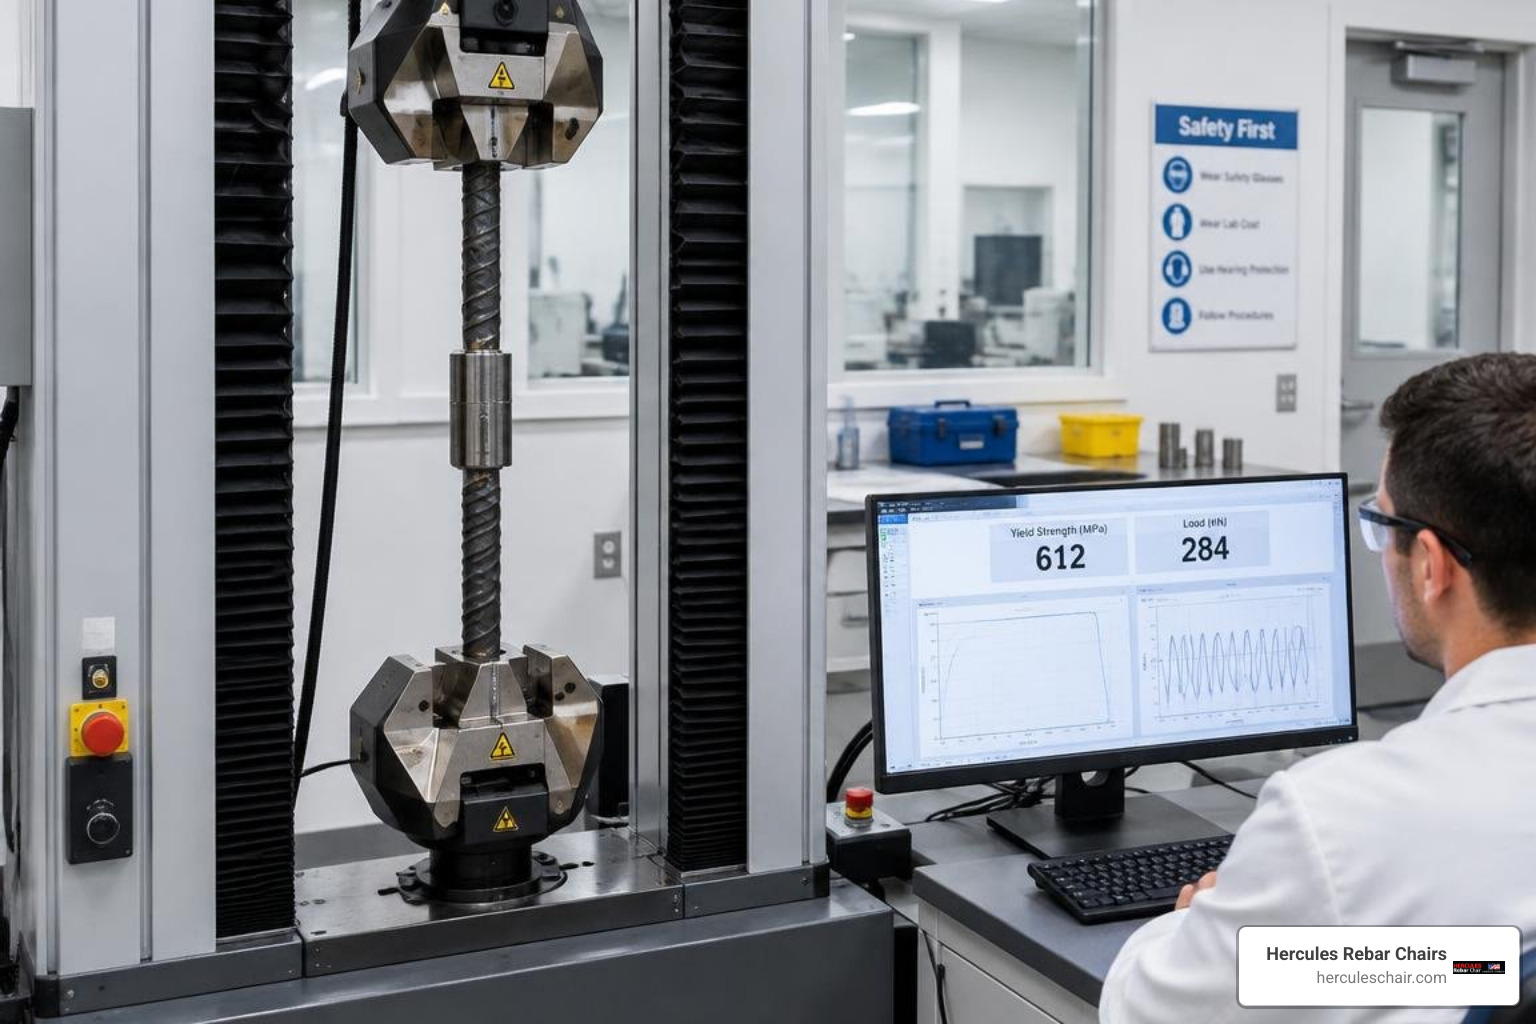
Leading fabricators test their product lines to international codes to verify consistent yield, tensile, and slip limits:
- ACI 318 (Building Code Requirements for Structural Concrete): Mandates Type 1 couplers develop at least 125% of the specified yield strength, and Type 2 couplers develop the full specified tensile strength of the spliced bar.
- ASTM A615 / ASTM A706: Governs raw billet steel and low-alloy weldable deformed rebar compatibility.
- ISO 15835: Outlines international testing protocols for mechanical splices under static, cyclic, and dynamic fatigue conditions.
- IS 16172:2023: Specifies rigorous mechanical splice parameters, categorizing connections into distinct performance classes.
- ISO 9001:2015: Guarantees systematic quality management and traceability throughout manufacturing.
Reviewing a comprehensive contractor guide to rebar couplers and sleeves helps field teams verify third-party certifications before parts arrive on site.
Understanding Class L vs Class H Couplers for Seismic Demands
Standards like IS 16172:2023 categorize mechanical couplers into distinct performance tiers:
- Class L (Standard Static Load Couplers): Designed for general structural framing where loading is predominantly static or moderate. These couplers achieve full tensile capacity (typically 125% to 135% of yield) with standard slip tolerances, making them ideal for foundations, gravity slabs, and light commercial frames.
- Class H (High-Demand Seismic Couplers): Built for high-ductility seismic zones, heavy bridge piers, and high-rise columns. Class H couplers undergo severe low-cycle reverse tension-compression testing to confirm they maintain structural grip under plastic deformations without brittle fractures. They match high-strength grades such as Fe 500, Fe 550, and ASTM A706 Grade 60 or 80.
Jobsite Installation, Tooling, and Quality Assurance Protocols
Even a top-tier coupler will fail if it is improperly installed on the jobsite. Consistent quality assurance procedures bridge the gap between laboratory certifications and field performance.
Field Installation Equipment and Torque Verification
Follow these field steps to ensure code-compliant connections:
- Inspect Threads: Check bar ends and coupler interiors for dirt, rust, concrete splatter, or deformed thread ridges.
- Hand Thread to Engagement: Spin the coupler fully onto the fixed bar until it bottoms out on the internal center stop.
- Align Spliced Bar: Align the secondary bar axially to prevent cross-threading.
- Apply Specified Torque: Use a calibrated torque wrench to tighten the joint to the manufacturer’s specified foot-pound value.
- Verify Bolt Shearing (For Bolted Types): When using lock-shear systems, drive the bolts sequentially until every hex head shears off flush with the sleeve surface.
For complete field workflows, consult this guide on how to install rebar couplers correctly.
Product Traceability and Defect Prevention
Full traceability prevents non-compliant steel from getting embedded in structural pours. Quality-focused manufacturers stamp every individual coupler with its batch heat number, diameter sizing, and load class.
Match physical sleeve markings against supplied Mill Test Reports (MTRs) and third-party laboratory tensile certifications. Couplers must also ship with protective end caps to shield precision threads from damage and rust during transit.
Frequently Asked Questions About Rebar Couplers
What is the difference between Class L and Class H couplers?
Class L couplers meet standard tension and compression requirements for conventional static structures. Class H couplers undergo specialized cyclic fatigue and reverse tension-compression testing to ensure ductile performance in high-stress seismic framing, bridges, and critical infrastructure.
How do rebar couplers reduce construction costs compared to lap splicing?
Couplers eliminate the 40d to 60d overlap lengths needed for lap splices, cutting overall rebar tonnage. They also ease congestion in dense column-beam joints, which eliminates concrete consolidation issues, speeds up formwork placement, and lowers crane hoisting weights.
What tools and equipment are required for rebar coupler installation?
Threaded couplers require calibrated torque wrenches, thread gauges, and bar-end preparation machines (such as cold-upset forging presses or rib-peeling thread rollers). Bolted shear systems only need standard impact drivers equipped with hex sockets to tighten bolts until their heads shear off.
Conclusion
Securing dependable structural continuity across your concrete pours comes down to partnering with a verified manufacturer and maintaining strict on-site quality control. Coupling systems eliminate congestion, cut rebar tonnage, and create direct axial load paths that keep structures safe under heavy static and seismic loads.
When preparing your reinforcement layouts, proper steel placement goes hand-in-hand with stable positioning. We at Hercules Rebar Chairs (T.J. Harris Co.) manufacture the durable red concrete supports that crews rely on nationwide. Backed by 14 million units sold across the United States, our American-made chairs keep rebar cages secure, stable, and code-compliant.
Explore premium rebar splicer and coupling solutions to streamline structural connections on your next pour.